In electronics manufacturing, detecting a potential defect is only part of the quality control process. Manufacturers must also determine whether inspection results are accurate, repeatable, and reliable enough to support production decisions. This is particularly important in high-mix printed circuit board assembly (PCBA), where different board designs, component packages, and soldering requirements may pass through the same production line.
X-ray inspection provides visibility into solder joints and other internal structures that cannot be fully evaluated through conventional visual inspection alone. However, image interpretation, inspection settings, component geometry, and operator judgment can all influence the results.
This guide explains how electronics manufacturers can validate X-ray inspection results, reduce false calls, and establish a repeatable inspection process.
X-ray inspection is widely used to examine hidden features in electronic assemblies, including solder joints beneath ball grid array (BGA) packages, bottom-termination components, and other areas that are difficult to access optically.
Effective x ray electronics inspection requires more than producing a clear image. The inspection process must reliably distinguish acceptable conditions from defects that require investigation.
Three common challenges are particularly important.
False positives: An acceptable solder joint may be incorrectly flagged as defective, resulting in unnecessary rework and additional inspection.
False negatives: A real defect may not be identified, allowing a potentially nonconforming assembly to proceed.
Inconsistent interpretation: Different operators or inspection settings may produce different conclusions from similar images.
Validation helps manufacturers understand these limitations and establish consistent decision criteria. It also creates a documented basis for evaluating inspection performance when products, components, or production processes change.
Validation should cover the complete inspection workflow rather than focusing exclusively on the X-ray machine.
The image must provide sufficient contrast and resolution to evaluate the feature of interest. Component thickness, material overlap, magnification, viewing angle, and acquisition settings can influence visibility.
A visually attractive image is not automatically sufficient for defect detection. The relevant solder joint or internal feature must be distinguishable enough for the intended evaluation.
Manufacturers should identify which defects the inspection process is intended to detect. These may include solder bridging, voiding, insufficient solder, or other application-specific abnormalities.
The validation method should use representative samples and clearly defined acceptance criteria.
Repeated inspections of the same sample under equivalent conditions should produce consistent results. Significant variation may indicate problems with image settings, fixture positioning, inspection procedures, or interpretation criteria.
Where inspection involves human interpretation, operators should use consistent criteria and receive appropriate training. Reference images and documented defect examples can help reduce differences between inspectors.
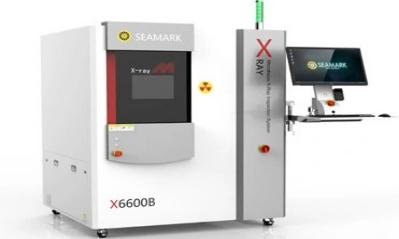
A structured procedure makes inspection performance easier to evaluate and maintain.
Start with the applicable product specifications, customer requirements, and relevant industry standards. Define which conditions are acceptable, which are defective, and which require further review.
For example, solder voiding criteria may depend on the component type, joint geometry, applicable standard, and customer specification. A single universal threshold should not be assumed for every assembly.
Use known-good samples and samples containing confirmed defects wherever possible. Include representative component packages, board layouts, and solder joint geometries.
Reference samples should reflect the actual products being inspected rather than relying entirely on generic images.
Document relevant parameters, such as X-ray energy, image acquisition settings, magnification, viewing angle, and fixture positioning.
The appropriate settings depend on the inspection target and equipment configuration. They should be established through testing rather than copied indiscriminately between different products.
Compare inspection findings with verified reference results. Depending on the defect and application, this may involve expert review, complementary inspection methods, or destructive analysis of selected samples.
The objective is to determine whether the X-ray result correctly represents the feature being evaluated.
Document false calls, inconsistent results, and cases requiring additional review. Investigate whether the cause relates to image quality, inspection settings, component geometry, or unclear acceptance criteria.
This information can guide improvements to the inspection process.
Choosing the appropriate inspection configuration also affects how validation is performed.
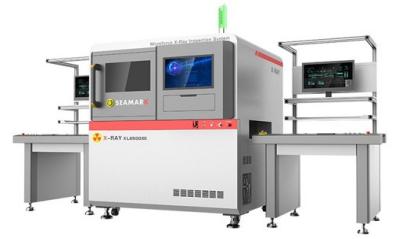
Inline X-ray automated inspection integrates X-ray inspection into a production line. Boards can be inspected as part of the manufacturing workflow, supporting automated handling and consistent inspection sequences.
Inline systems are useful when production volume, inspection frequency, and cycle-time requirements justify line integration. Validation should consider inspection coverage, throughput, board handling, recipe management, and how failed inspections are flagged for review.
By comparison, offline inspection generally involves moving boards or samples to a dedicated inspection station. This arrangement can provide greater flexibility for engineering analysis, troubleshooting, sample evaluation, and products that do not require inspection on every production cycle.
Neither approach is universally superior. The right configuration depends on production volume, product mix, inspection objectives, available space, and the required response time.
High-mix PCBA manufacturing introduces additional challenges because different products may require different inspection recipes and acceptance criteria.
Manufacturers can improve consistency by maintaining controlled product-specific settings, version-controlled inspection programs, and clear procedures for introducing new board designs.
When a new component package or PCB layout is introduced, the inspection process should be reviewed to confirm that the selected settings remain suitable.
Periodic revalidation may also be appropriate after major equipment maintenance, software changes, inspection recipe updates, or significant production process changes.
Where automated defect recognition is used, manufacturers should verify its performance on representative products and periodically review cases that require manual intervention.
Useful indicators include:
False-positive rate
False-negative rate, where reliably measurable
Repeatability of inspection results
Percentage of boards requiring manual review
Inspection cycle time
Discrepancies between X-ray findings and confirmed reference results
Frequency of inspection recipe adjustments
These metrics should be interpreted in context. For example, a lower manual review rate is not necessarily an improvement if defect detection performance deteriorates.
The goal is to balance reliable defect identification, efficient throughput, and consistent decision-making.
Validating X-ray inspection results is essential for maintaining reliable quality control in high-mix PCBA manufacturing. Image quality, defect detection capability, repeatability, operator consistency, and documented acceptance criteria all influence inspection performance.
Whether a factory uses inline X-ray automated inspection or offline inspection, the validation process should be based on representative samples, verified reference evidence, controlled settings, and documented results.
By establishing a structured validation procedure for x ray electronics inspection, manufacturers can reduce inconsistent judgments, improve confidence in inspection results, and make better-informed production decisions.
Validation helps determine whether the inspection process consistently identifies relevant defects and distinguishes them from acceptable conditions. It can reduce false calls and improve confidence in quality decisions.
Ideally, manufacturers should use representative known-good samples and confirmed defect samples covering the component packages, board designs, and defects relevant to their production.
Inline inspection is integrated into the production line and supports automated board handling. Offline inspection uses a separate station and is often suitable for engineering analysis, troubleshooting, and flexible inspection requirements.
No. Detectability depends on the defect type, material structure, geometry, image quality, equipment capabilities, and inspection settings. Some defects require complementary inspection methods.
Revalidation frequency should follow the manufacturer's quality procedures and applicable requirements. It may also be necessary after major maintenance, software changes, new product introductions, or significant process changes.
NEXT
 EN
 es
 ko
 de
 it
 pt
 th
 ar
 pl
 vi
 tr
 ru