Accurate incoming inspection is essential for electronics manufacturers that rely on a stable supply of surface-mount components. When component reels arrive at a warehouse, the quantities recorded on supplier labels, packing lists, and purchase orders may not always match the actual inventory. If these discrepancies remain unresolved, they can lead to stock inaccuracies, production delays, and unnecessary purchasing costs.
An X ray reel counter helps manufacturers verify the quantity of components inside a reel without manually unwinding and counting individual parts. By incorporating automated counting into incoming inspection procedures, SMT factories can improve quantity verification and establish more consistent records.
This article explains why reel quantity discrepancies occur, how to investigate them, and how an offline counter or counter machine online solution can support supplier incoming inspection.
Component quantity discrepancies can arise at different stages of the supply chain. Identifying the potential cause helps purchasing and warehouse teams determine the appropriate corrective action.
Supplier labels and packing lists provide important inventory information, but the recorded quantity should not automatically be treated as a verified physical count.
For example, a reel may be labeled with an expected quantity that does not reflect its current contents. This can happen when material is repackaged, reels are partially used, or inventory records are updated incorrectly.
An X-ray reel counter can help receiving personnel compare the actual estimated component quantity with the documented quantity before the material enters available inventory.
Not every reel received by an electronics manufacturer contains a standard full quantity. Partial reels may be supplied for smaller orders, returned from previous production runs, or repackaged during material handling.
These situations require careful identification because the expected quantity may differ from the standard packaging quantity. The receiving team should confirm the reel's status and compare the counting result against the appropriate reference rather than assuming that every reel is full.
Discrepancies can also result from incorrect data entry, inaccurate return records, or mistakes during warehouse transfers.
In these cases, a physical count can help establish the actual quantity, but it does not independently explain why the discrepancy occurred. Purchasing, warehouse, and supplier quality teams should review transaction records to determine the underlying cause.
An X-ray reel counter uses X-ray imaging and image-processing techniques to estimate the number of components inside a reel. This allows operators to verify quantities without manually counting each component.
A standardized incoming inspection process can follow five steps.
Step 1: Verify the reel identity. Check the part number, supplier label, lot information, and purchase order before counting.
Step 2: Establish the expected quantity. Review the packing list and relevant supplier documentation. Confirm whether the reel is expected to be full, partial, or repackaged.
Step 3: Perform the count. Use an X ray reel counter that supports the component and reel format. Follow the equipment's recommended operating procedure.
Step 4: Compare the results. Record the expected quantity, measured quantity, and any difference. Repeat the count or perform an additional verification when results are uncertain.
Step 5: Record the inspection decision. Release the material, hold it for further investigation, or initiate a supplier discrepancy report according to the factory's quality procedures.
For example, if the documentation lists 3,000 components but the counter reports a different quantity, the receiving team should first confirm the reel identity and counting conditions. If the difference remains, the material may need to be held while the supplier and purchasing team investigate.
This procedure helps distinguish a genuine quantity discrepancy from a counting or documentation error.
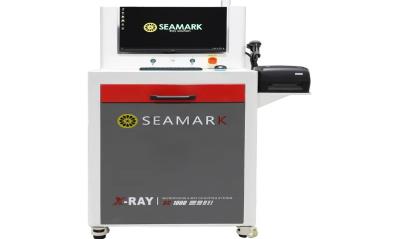
The appropriate equipment configuration depends on how materials move through the receiving and warehouse processes.
An offline counter is generally used at a dedicated workstation. Operators bring selected reels to the machine, perform the count, and record the results. This arrangement can suit incoming inspection, supplier discrepancy investigations, inventory audits, and partial-reel verification.
A counter machine online may be suitable when counting needs to form part of a more integrated material-handling workflow. Buyers should confirm the actual loading and unloading method, supported reel formats, throughput, and available software interfaces because online configurations can differ.
| Evaluation factor | Offline counter | Counter machine online |
|---|---|---|
| Typical application | Receiving checks and separate verification tasks | More integrated counting workflows |
| Material handling | Reels are brought to a counting workstation | Depends on the configured transfer and loading process |
| Deployment | Often flexible for standalone use | Requires assessment of workflow and integration requirements |
| Data recording | Manual or supported digital recording | Depends on available software and interfaces |
| Key selection factor | Counting-station capacity and operator workflow | Throughput, compatibility, and integration needs |
Neither configuration automatically guarantees better inventory accuracy. The result also depends on correct reel identification, verified counting performance, and reliable recording of inspection outcomes.
A reliable discrepancy process should produce records that purchasing and supplier quality teams can use for investigation and corrective action.
For every unresolved difference, record:
Supplier name and shipment reference.
Component part number and reel identification.
Expected quantity and measured quantity.
Absolute quantity difference.
Counting method and verification result.
Inspection date and responsible operator.
Investigation findings and final disposition.
The absolute quantity difference can be calculated as:
Quantity difference = Measured quantity − Expected quantity
A negative result indicates that the measured quantity is lower than expected, while a positive result indicates that it is higher.
If discrepancies recur with the same supplier or component type, review the historical records to identify patterns. Repeated differences may indicate problems with packaging control, labeling, transaction records, or counting procedures.
It is also important to distinguish quantity verification from authenticity inspection. An X-ray counter estimates the quantity of reel contents; it does not independently confirm that every component is genuine, correctly identified, or electrically functional.
Yes. It can estimate the actual component quantity for comparison with the documented quantity, provided the reel and component type are supported by the equipment.
Not necessarily. The receiving team should verify the reel identity, repeat the count when appropriate, and investigate the discrepancy according to the company's incoming inspection procedure before deciding on rejection or acceptance.
Yes. An offline counter can be suitable when reels are counted at a dedicated workstation and the equipment's capacity meets the receiving workload.
Only when the equipment and connected systems support the required interfaces and have been configured accordingly. Buyers should confirm these capabilities with the supplier before purchase.
No. Quantity counting and component authentication are different tasks. Authenticity assessment may require supplier traceability checks, packaging inspection, electrical testing, or other appropriate verification methods.
Supplier reel quantity discrepancies can undermine inventory accuracy and disrupt electronics manufacturing if they are not identified and resolved promptly. An X ray reel counter provides a practical method for verifying component quantities during incoming inspection and comparing physical counts with supplier documentation.
Choosing between an offline counter and a counter machine online depends on material flow, counting volume, and integration requirements. By combining appropriate counting equipment with clear discrepancy procedures, accurate inspection records, and supplier follow-up, SMT manufacturers can strengthen incoming quality control and maintain more reliable component inventories.
 EN
 es
 ko
 de
 it
 pt
 th
 ar
 pl
 vi
 tr
 ru